 EN
Topic: Busbar cutting / shearing · quality metrics · buying tips for Australian workshops
Brand focus: LT / LTMC 303U-3-C · 503U-3-C · 803U-3-C
Audience: Australian switchboard builders and panel shops
Quick answer
A busbar cutting (shearing) machine — standalone or as the shear station on a 3-in-1 such as the LT 303U-3-C / 503U-3-C / 803U-3-C — should be chosen from material, finished-length tolerance, squareness, burr limit, deformation, and production pattern, not catalogue max thickness alone. Poor cut edges create rework in punching, bending, assembly, and inspection in Australian panel shops. Prove quality with documented FAT / continuous cut samples, not a single showpiece.
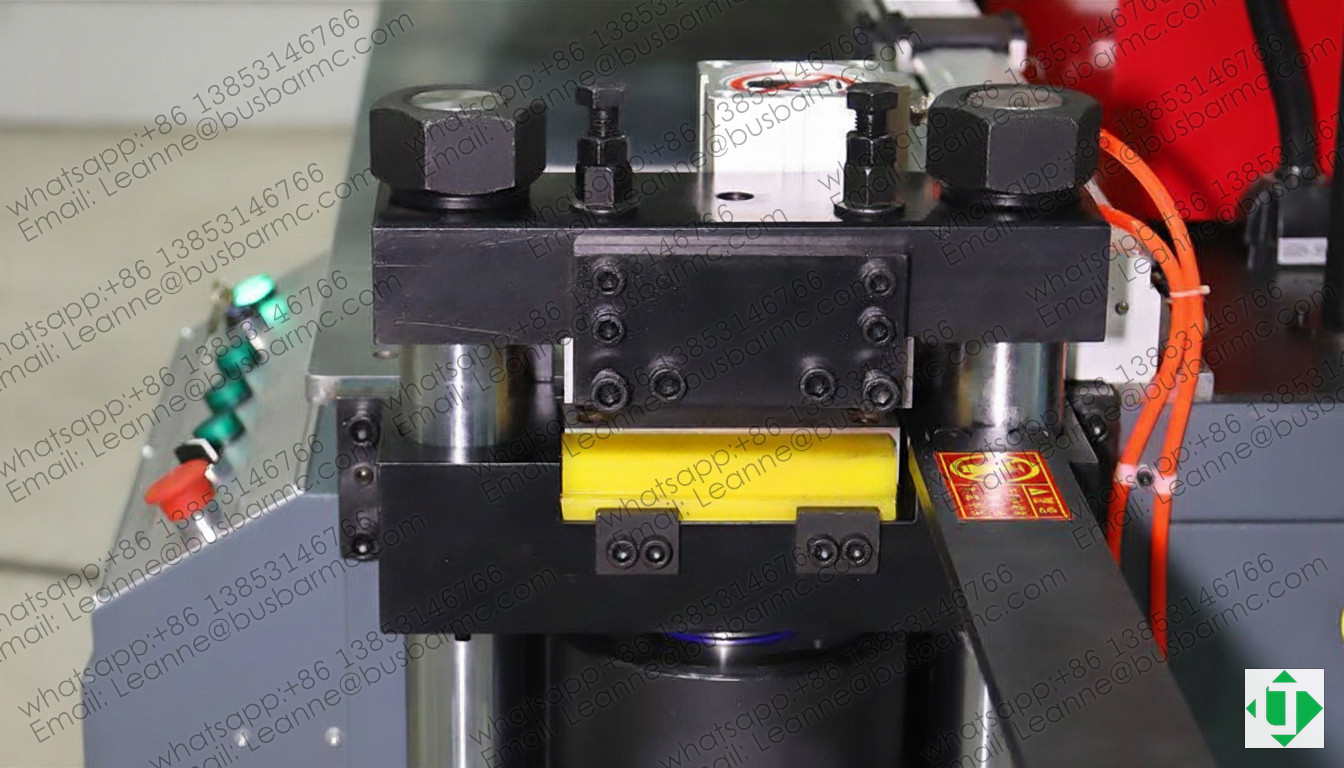
Cutting (shearing) unit close-up (LT / LTMC)
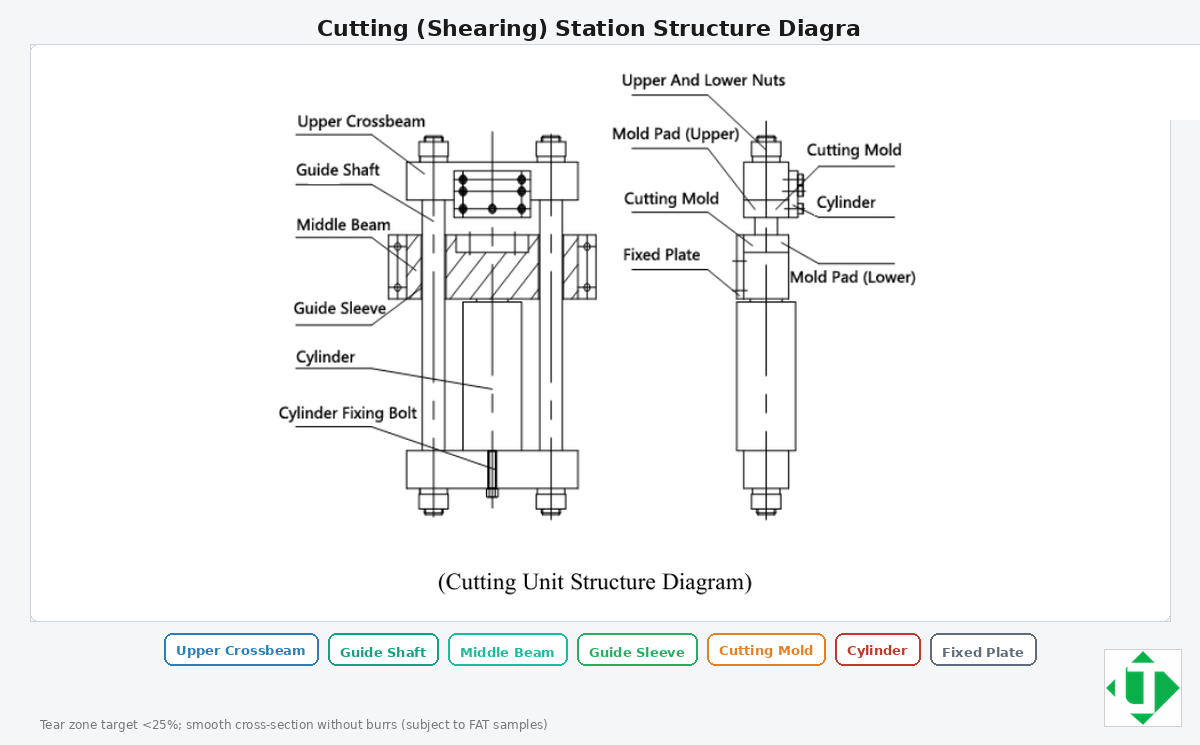
Cutting station structure diagram (EN)
What specifications to confirm before buying
| Specification | Why it matters |
|---|---|
| Material grade (Cu / Al / laminated) | Cutting load and blade choice |
| Temper | Burr, wear, force |
| Width × thickness | Capacity + clearance |
| Raw bar length | Table / roller support |
| Finished length tolerance | Manual stop vs servo / CNC |
| Burr limit | Blade quality + process capability |
| Squareness | Downstream bend / weld / fit |
| Surface / film | Hold-down marks |
| Cycle time | Automation level |
| Positioning method | Manual / servo / CNC |
| Blade spare lead time | Downtime risk |
Cutting methods vs positioning systems
Evaluate how the bar is separated separately from how length is positioned.
Shearing (hydraulic blade)
Common for copper/aluminium busbars: short cycle, limited chips. Edge quality depends on clearance, sharpness, alignment, clamp, and support. Wrong clearance → burrs and local deformation.
Saw cutting
Consider when end profile or material condition makes shearing unsuitable. Expect chips, kerf loss, and often longer cycle time. Compare blade life and secondary finishing—saw is not automatically “higher quality.”
Manual stop vs servo / CNC positioning
| Positioning | Best fit | Watch-out |
|---|---|---|
| Manual stop / scale | Mixed low volume | Operator variation |
| Servo length stop | Recurring lengths | Travel + dead zone |
| CNC program recall | Multi-length kits | Revision control |
Finished-cut results to inspect
Agree before FAT: tolerance, instrument, sample quantity, measure points, inspector, acceptance method.
Inspect: finished length, squareness, max burr height, end deformation, surface damage. For continuous tests, record consecutive parts—not one selected sample—in the FAT pack.
Where cutting sits on a 3-in-1
On LTMC U-3-C machines the shear shares the frame with punch and bend, with independent pump groups so stations can run in parallel when staffed.
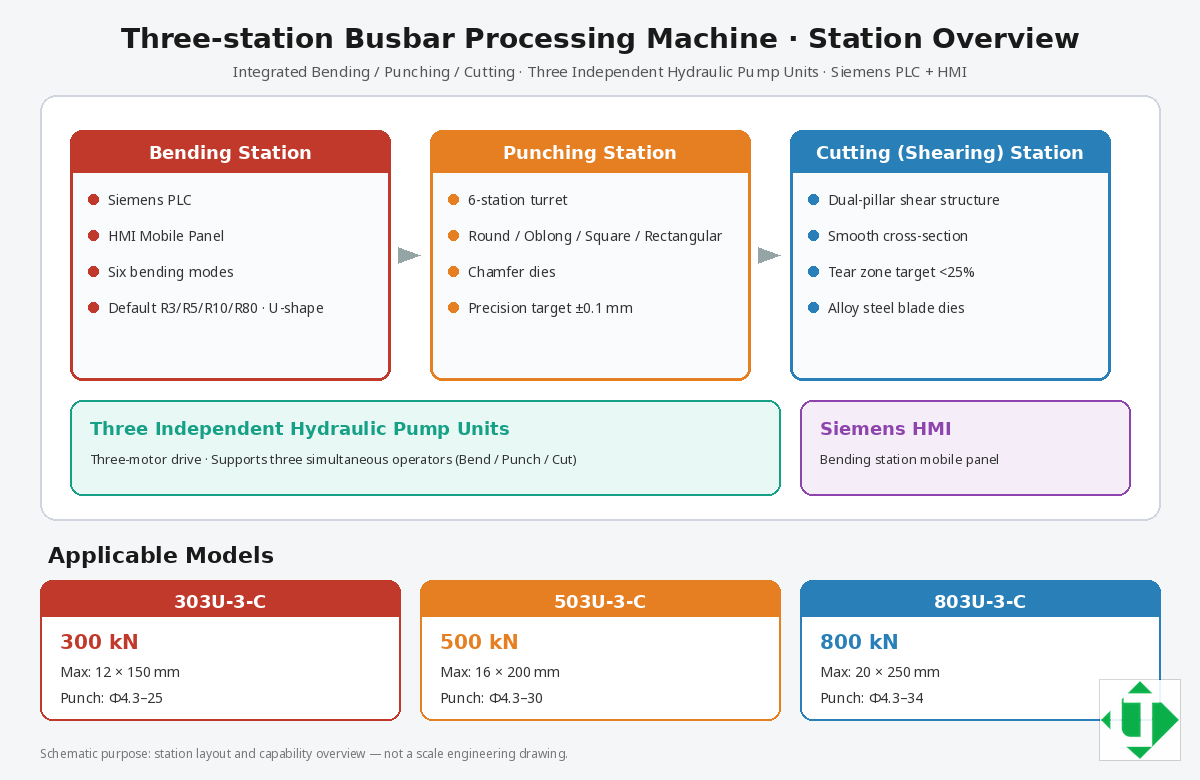
Three-station layout overview with English callouts
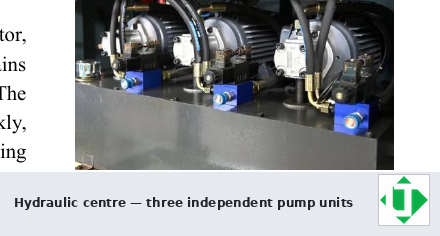
Hydraulic centre: three independent pump units
Published shear envelopes track model class: about 12×150 (303) · 16×200 (503) · 20×250 (803) mm—confirm width wording on OA.
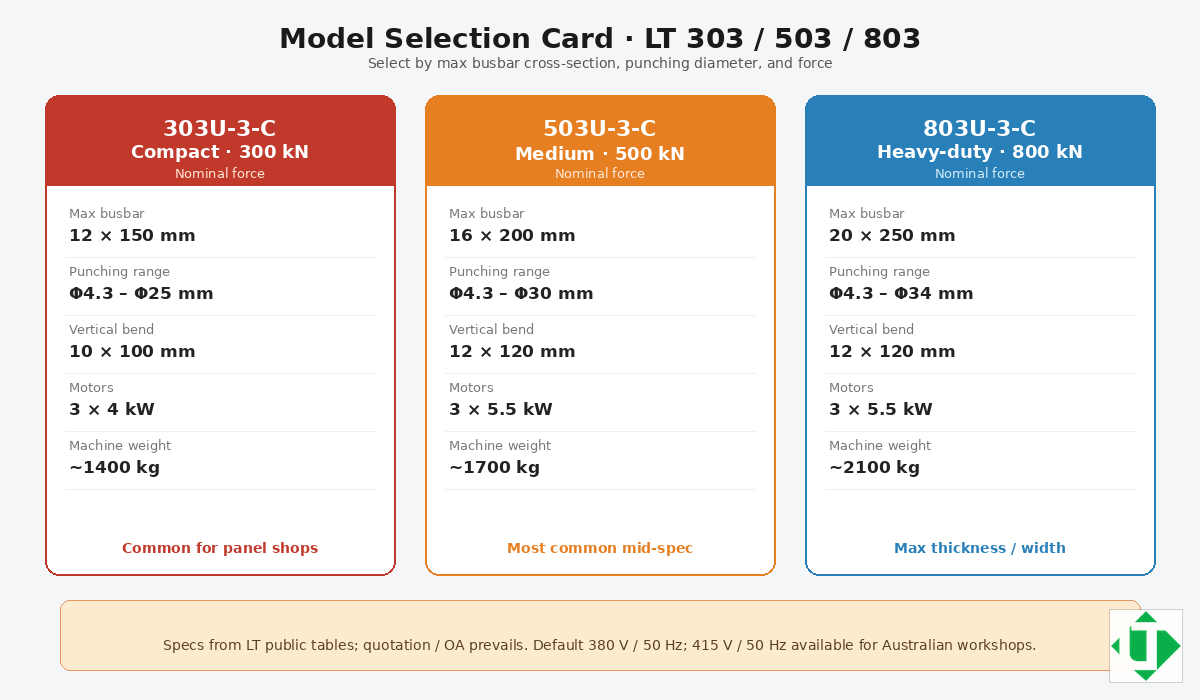
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
Buying tips (decision cues)
- Write acceptance numbers for length / square / burr before RFQ.
- Ask for blade material, clearance guidance, and spare lead time.
- Match positioning to how often lengths repeat.
- If most jobs also punch+bend, prefer a sized 3-in-1 over a lonely shear—unless cutting is the bottleneck.
- Require FAT with your representative section, not only brochure copper.
FAQ
What is a busbar cutting machine?
Equipment that shears or saws copper/aluminium busbars to drawing length with controlled edge quality.
Shear or saw?
Shear for most flat Cu/Al production; saw when the drawing or material rejects shearing. Compare cycle, kerf, chips, and finishing.
Can the shear on a 3-in-1 replace a dedicated cutter?
Often yes for SME mixed work. Choose dedicated cutting when cut hours/day justify a separate station or automatic feed line.
How do I judge cut quality?
Measure length, squareness, burr, deformation, and surface—on multiple consecutive parts under agreed instruments.
What LTMC models cover cutting?
303U-3-C / 503U-3-C / 803U-3-C include hydraulic shear stations sized to the table above.
Talk to LT about a machine for your Australian workshop
For a quotation, FAT samples, tooling lists or sea freight to Australian ports (Sydney, Melbourne, Brisbane, Fremantle or Adelaide), contact LT at [email protected] or +86 13853146766 (WhatsApp), or use the contact page. Public product information is on busbarcnc.com.
Source and revision
- Prepared for: Australian switchboard builders and panel shops, published on busbarcnc.com
- Brand: LT / LTMC · models 303U-3-C · 503U-3-C · 803U-3-C
- Figures: LT / LTMC workshop photos and English schematics, hosted on this site
- Note: Confirm capacities, dies and voltages on the order acknowledgment and FAT samples. Electrical clearances in the finished assembly follow the switchgear design and AS/NZS 61439, not the machine alone.