 EN
Topic: Copper busbar machine selection · process route · tooling · FAT
Brand focus: LT / LTMC 303U-3-C · 503U-3-C · 803U-3-C
Audience: Australian switchboard builders and panel shops
Quick answer
A copper busbar machine may be one integrated 3-in-1 (LT 303U-3-C / 503U-3-C / 803U-3-C) or a set of dedicated punch, shear, and bend stations. For Australian switchboard and busduct work, start from the approved finished-part drawing: material temper, datums, holes/slots, finished length, bend lines, radii, short legs, and assembly interfaces. Confirm punching, shearing, and bending capacity separately — catalogue max size does not prove every operation on every geometry. Compare routes by complete cycle time, tooling, handling, first-article yield, and FAT evidence.
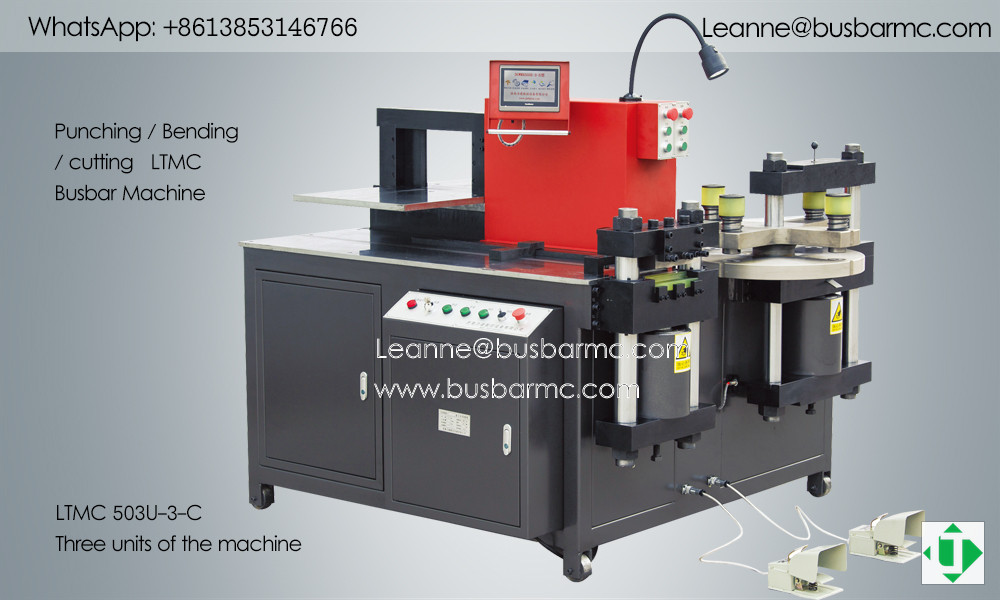
LTMC 503U-3-C three-station busbar machine overview (LT / LTMC)
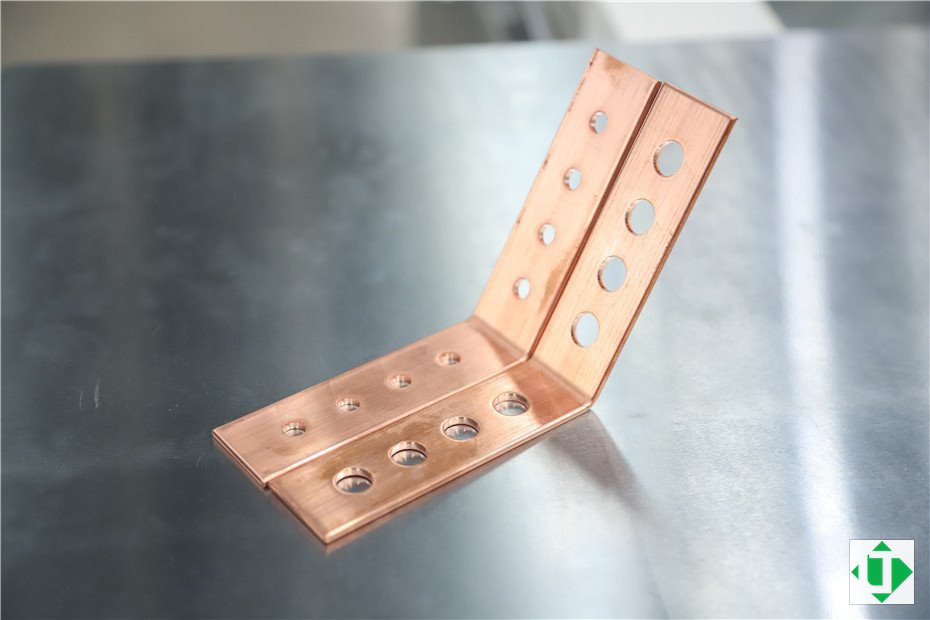
Copper samples after cut, punch and L-bend (LT / LTMC)
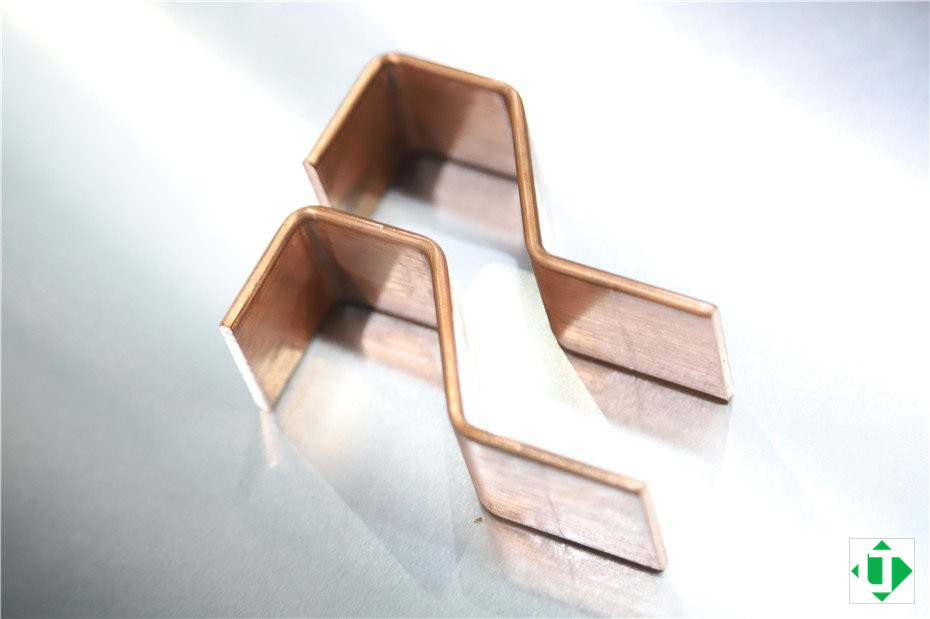
Copper Z / offset bend samples (LT / LTMC)
Copper applications that drive machine choice
| Application | What to review |
|---|---|
| Switchgear & panels | Hole layout, bend structure, cabinet clearances |
| Transformer connections | Section, terminal holes, surface, interface |
| Busduct / long runs | Length support, joints, volume |
| Energy storage / charging | Dense holes, compact bends, surface control |
Select from the finished-part family, not the application name alone.
Process route options
| Route | Best fit | Trade-off |
|---|---|---|
| Hydraulic 3-in-1 | Mixed copper kits, limited floor | Manual transfer between stations |
| CNC / servo-assisted 3-in-1 | Recurring copper drawings | Still one-frame capacity ceiling |
| Dedicated punch / shear / bend | High hours per process | More footprint |
| Automatic CNC line | High volume nesting | CapEx + floor |
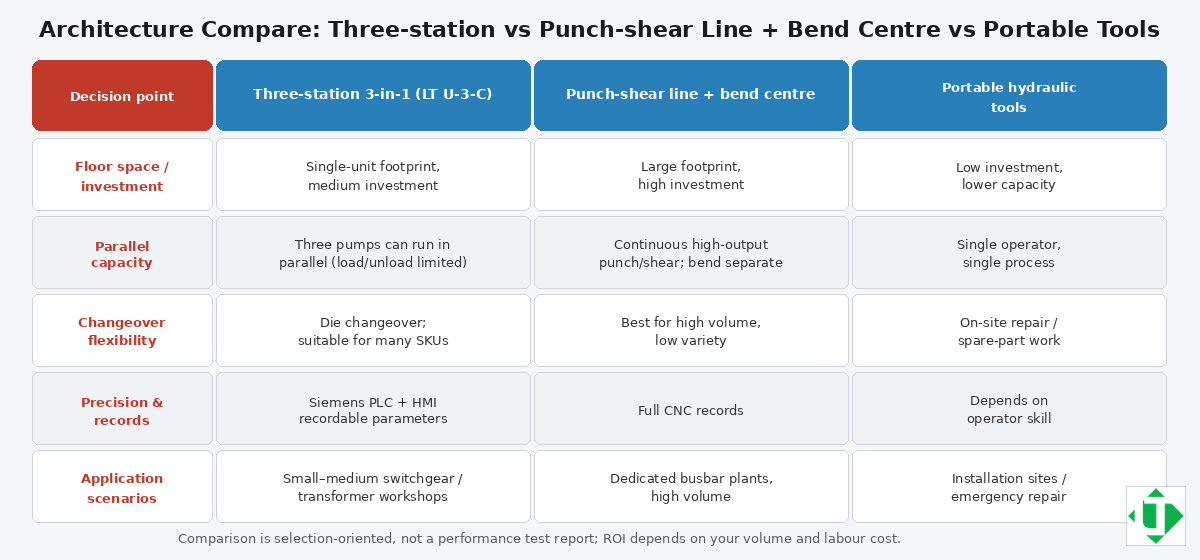
Architecture compare: 3-in-1 vs dedicated vs portable
Tooling that actually defines copper capability
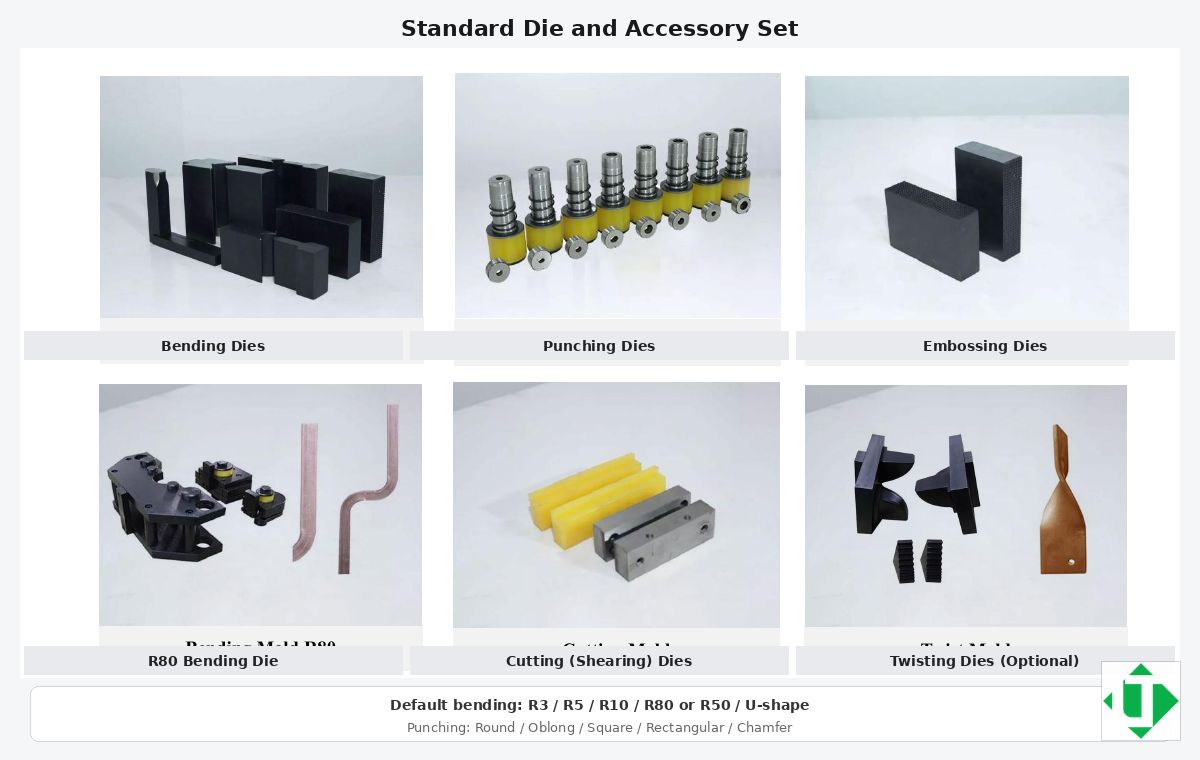
Standard die and accessory set with English labels
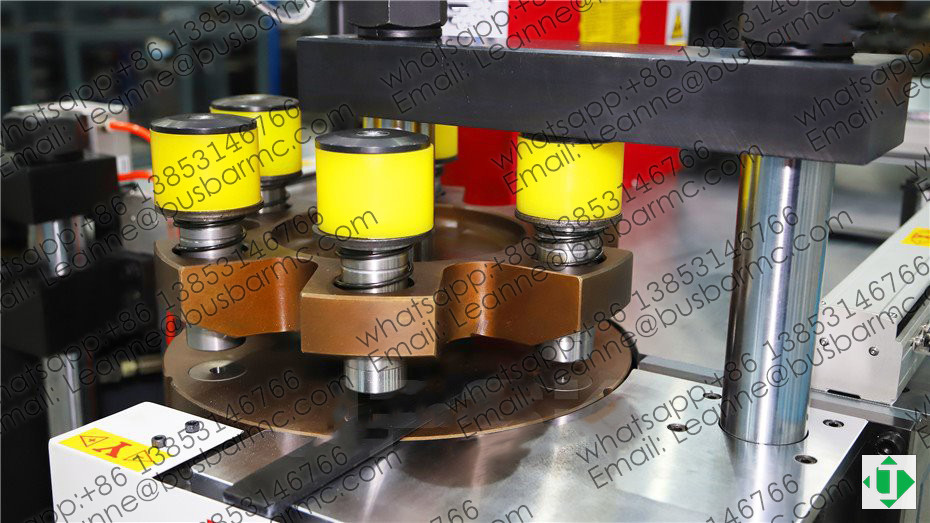
Punching turret unit with multi-station dies (LT / LTMC)
- Punch: round / oblong families; published ranges Φ4.3–25/30/34 by model
- Shear: blades + clearance for copper temper
- Bend: R3/R5/R10/R80 (or R50), U-dies; flat vs edge modes on Siemens HMI
- Optional emboss / twist only if ordered
Model card — size the copper envelope
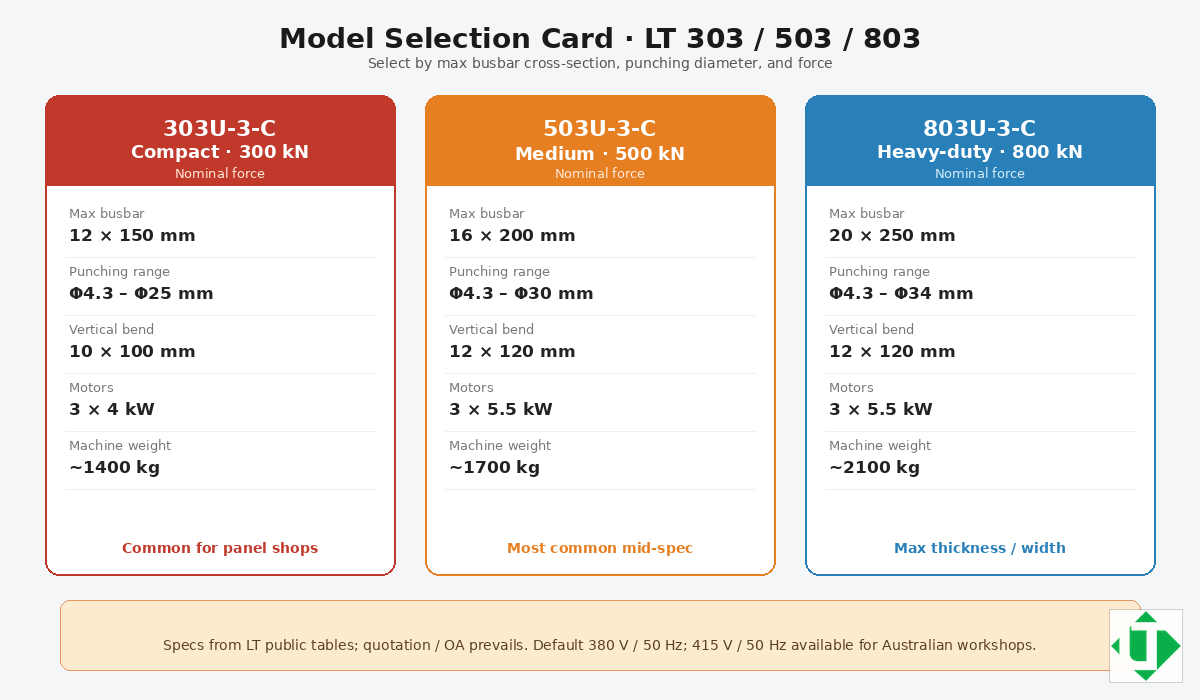
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
| Entity | 303U-3-C | 503U-3-C | 803U-3-C |
|---|---|---|---|
| Nominal force (kN) | 300 | 500 | 800 |
| Punching diameter (mm) | Φ4.3–Φ25 | Φ4.3–Φ30 | Φ4.3–Φ34 |
| Max thickness / width (mm) | 12 / 150 | 16 / 200 | 20 / 250 |
| Max horizontal bend (mm) | 150 / 12 | 200 / 16 | 250 / 20 |
| Max vertical bend size (mm) | 10×100 | 12×120 | 12×120 |
| Motor power | 3×4 kW | 3×5.5 kW | 3×5.5 kW |
Quick cue: 303 ≈ 12×150 / Φ25 · 503 ≈ 16×200 / Φ30 · 803 ≈ 20×250 / Φ34.
How to compare output fairly
Do not compare machines by stroke rate alone. Complete cycle time includes load, setup, tooling, position, punch, move, shear, bend, correct, unload, and inspect. Use the same copper drawing across suppliers; record operators, setup, conforming parts, rejects, and manual interventions.
RFQ package for copper machines
| Send | Used to confirm |
|---|---|
| Grade / temper / max section | Force & handling |
| Drawings (holes, bends, lengths) | Dies & sequence |
| Batch mix & output | 3-in-1 vs line |
| FAT criteria & instruments | Acceptance |
| Voltage / destination port (Sydney, Melbourne, Brisbane, Fremantle or Adelaide) | Electrical build |
FAQ
Can one machine cut, punch, and bend copper?
Yes—LTMC three-station models integrate all three. Throughput still depends on staffing and whether pumps run in parallel.
Is nominal force enough to select a copper machine?
No. Verify each station against your hardest hole, shear, and bend family.
What copper thickness can LTMC process?
Public tables: about 12 / 16 / 20 mm max thickness on 303 / 503 / 803—always pair with width and bend limits on the OA.
What should FAT include for copper?
Representative parts: length, hole positions, released bend angles, surface, and consecutive-part variation.
Talk to LT about a machine for your Australian workshop
For a quotation, FAT samples, tooling lists or sea freight to Australian ports (Sydney, Melbourne, Brisbane, Fremantle or Adelaide), contact LT at [email protected] or +86 13853146766 (WhatsApp), or use the contact page. Public product information is on busbarcnc.com.
Source and revision
- Prepared for: Australian switchboard builders and panel shops, published on busbarcnc.com
- Brand: LT / LTMC · models 303U-3-C · 503U-3-C · 803U-3-C
- Figures: LT / LTMC workshop photos and English schematics, hosted on this site
- Note: Confirm capacities, dies and voltages on the order acknowledgment and FAT samples. Electrical clearances in the finished assembly follow the switchgear design and AS/NZS 61439, not the machine alone.