 EN
Topic: Busbar punching · hole accuracy · dies · turret · positioning
Brand focus: LT / LTMC 303U-3-C · 503U-3-C · 803U-3-C
Audience: Australian switchboard builders and panel shops
Quick answer
Busbar punching quality is judged by finished hole position from the approved datum, hole size/profile, edge distance, burr, and deformation—not by machine positioning accuracy claims alone. On LT 303U-3-C / 503U-3-C / 803U-3-C machines, a multi-station turret plus adequate tonnage covers common round/oblong families when dies, clearance, and strippers match copper or aluminium temper. That positional discipline matters when the punched bar later sits in an Australian switchboard built to the workshop’s AS/NZS 61439 drawings.
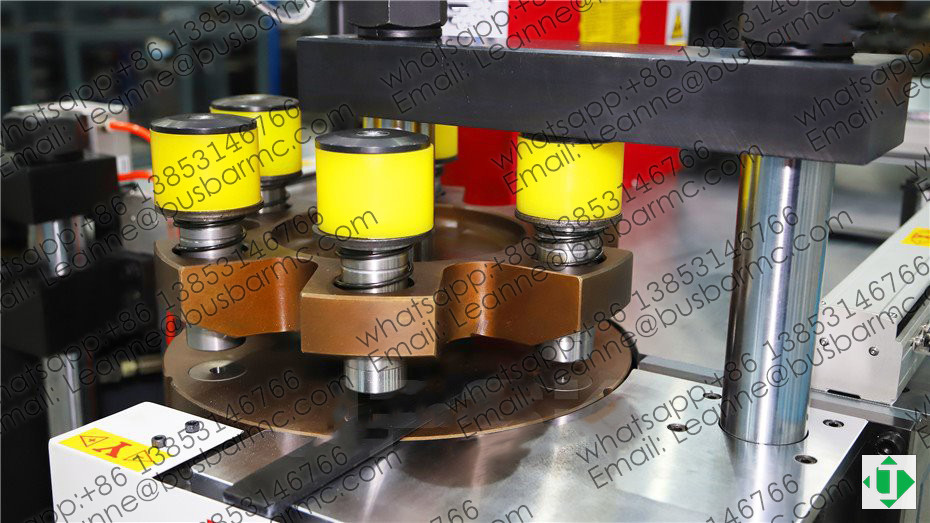
Punching turret unit with multi-station dies (LT / LTMC)
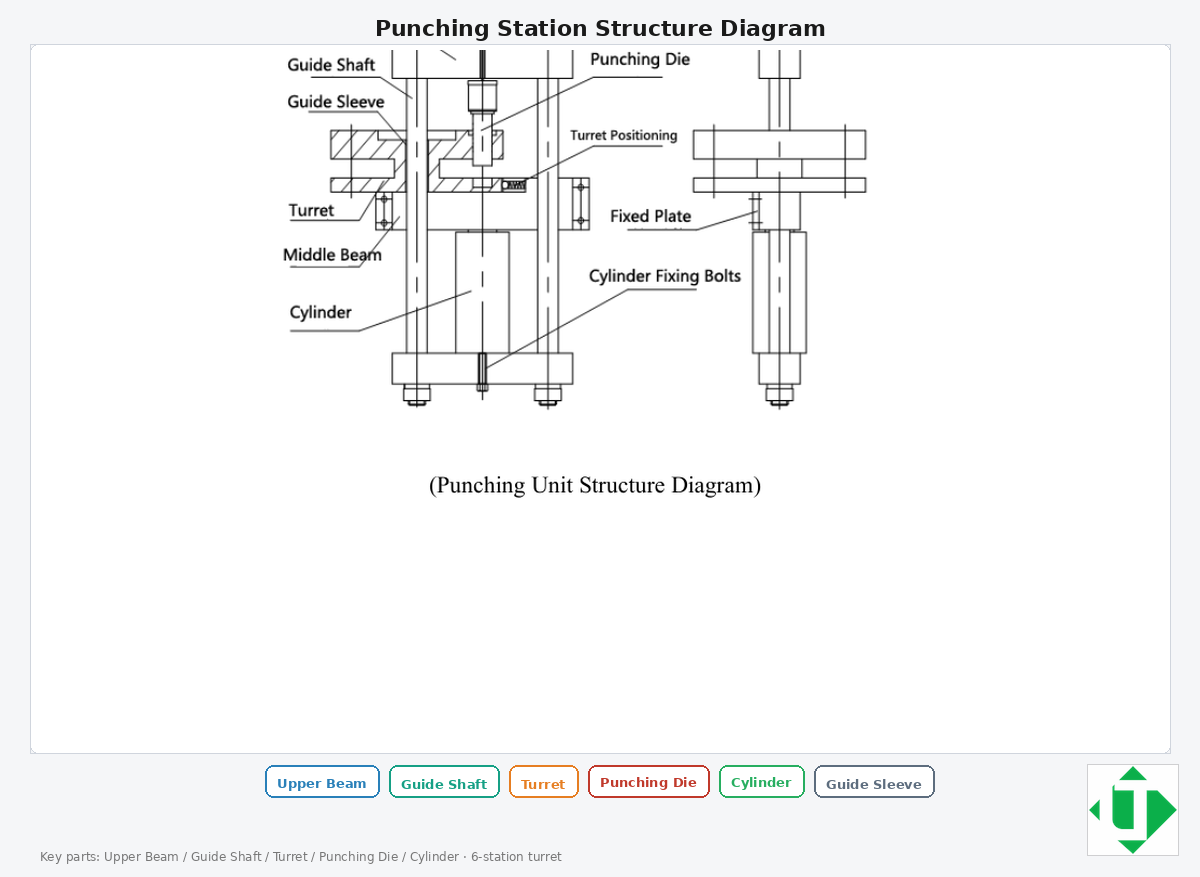
Punching station structure diagram (EN)
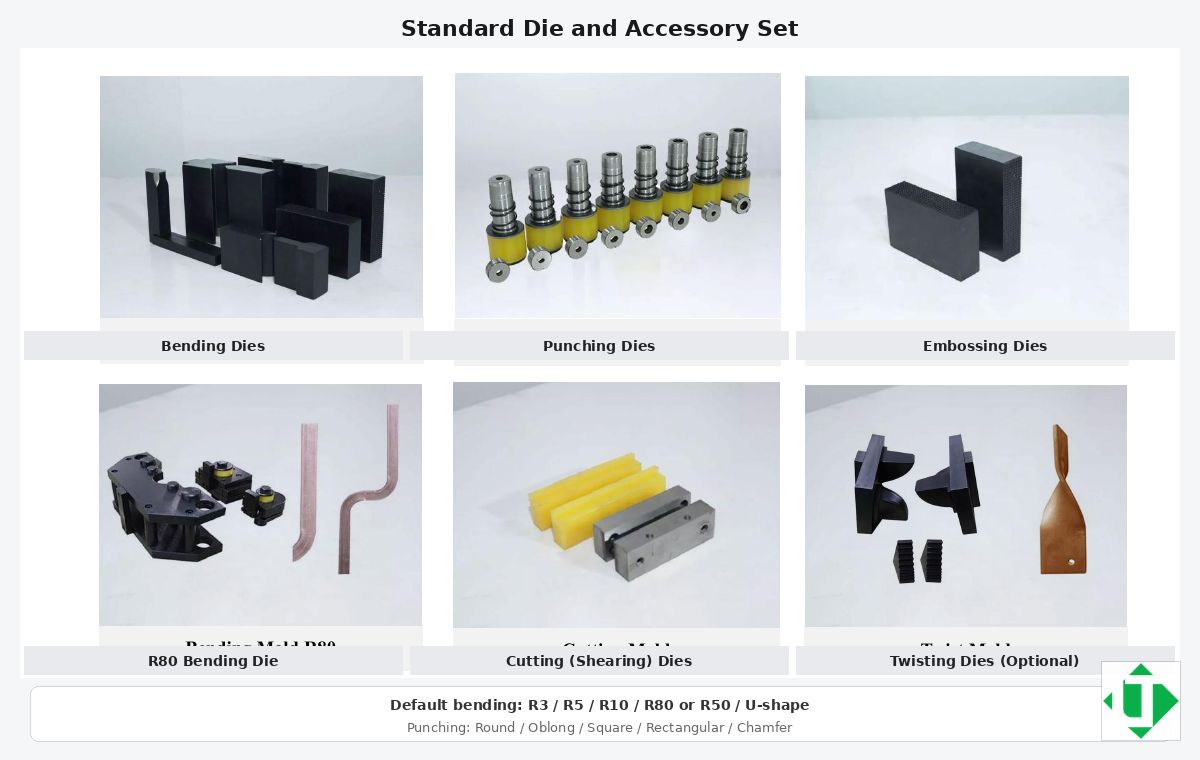
Standard die and accessory set with English labels
Define accuracy before you set up
| Drawing control | Why |
|---|---|
| Datum | All positions measured from here |
| Hole centre pitch | Kit fit to breakers / terminals |
| Edge distance | Die strength + standard compliance |
| Positional tolerance | Pass/fail for FAT |
| Profile (round/oblong/rect) | Die selection |
Verify finished holes from the drawing datum on multiple consecutive parts.
Dies, clearance, and turret practice
- Select dies for actual material, temper, thickness, and profile.
- Confirm punch/die clearance; re-check after Cu↔Al switches.
- Turret designs keep several dies centred for faster changeover.
- Illustrative starter families (confirm on order): round Ø7/9/11/13/17; oblong Ø11×15, Ø13×18, Ø17×21.
- Published ranges: 303 Φ4.3–Φ25 · 503 Φ4.3–Φ30 · 803 Φ4.3–Φ34.
After each die change: inspect burr, deformation, and edge quality before releasing the batch.
Positioning: manual vs servo / CNC
| Method | Helps when… | Still manual? |
|---|---|---|
| Scale / stop | Low mix | Yes |
| Servo axis | Recurring coordinates | Load / clamp often yes |
| CNC program | Multi-hole kits | Tool change / inspect |
Hydraulic punch force and CNC positioning can coexist—compare labour and repeatability, not slogans.
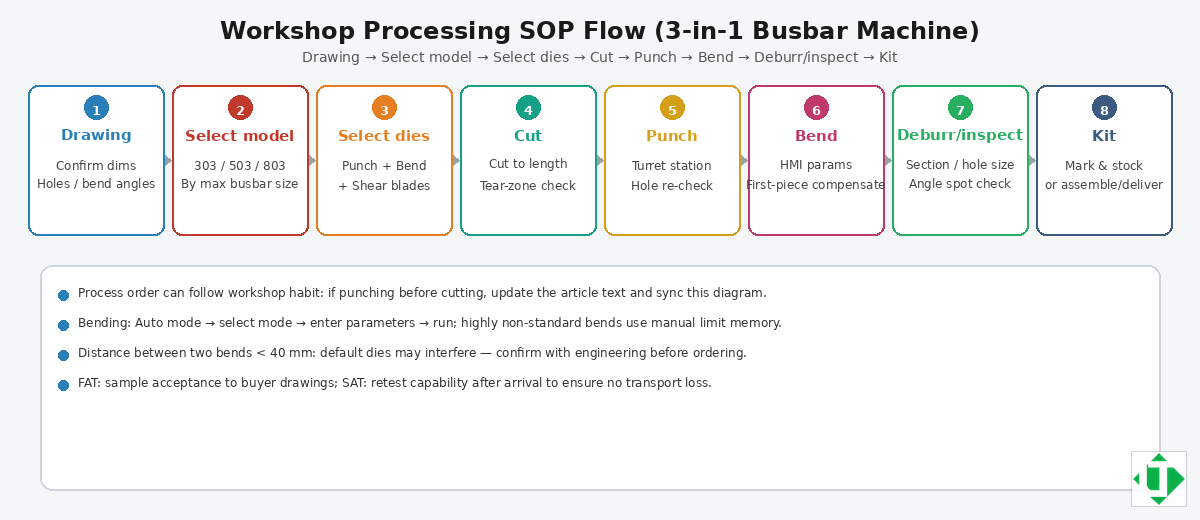
Workshop SOP flow: Drawing → Cut → Punch → Bend → Inspect
Model capacity for punching
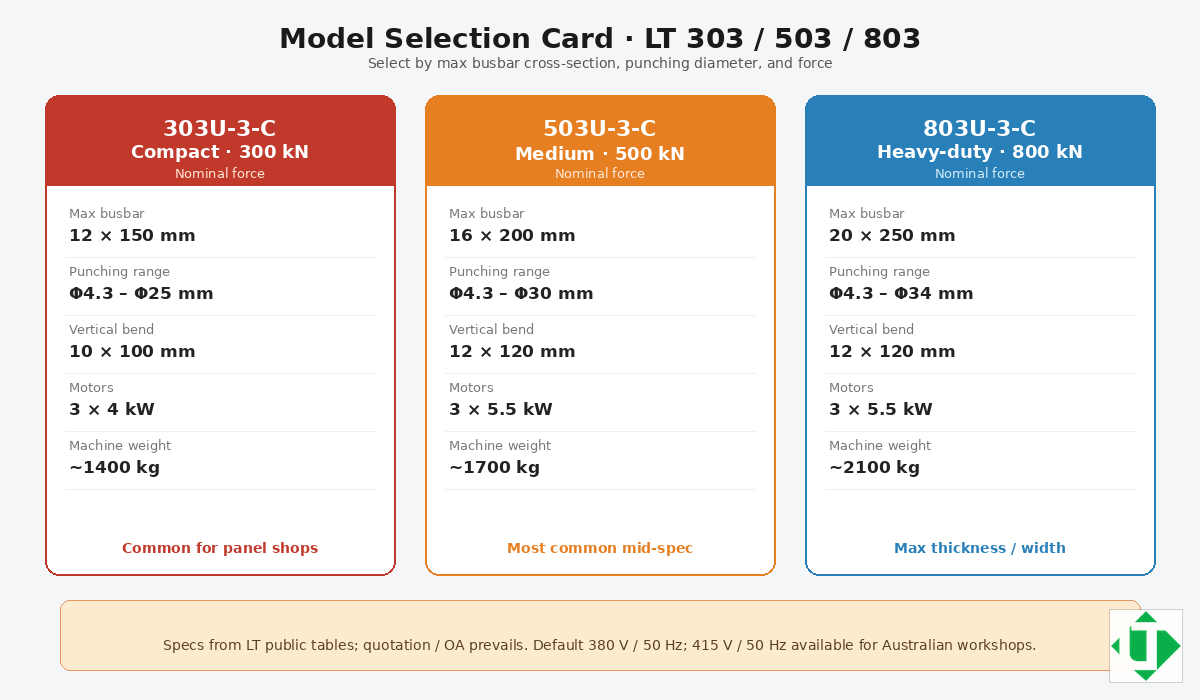
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
| Entity | 303U-3-C | 503U-3-C | 803U-3-C |
|---|---|---|---|
| Nominal force (kN) | 300 | 500 | 800 |
| Punching diameter (mm) | Φ4.3–Φ25 | Φ4.3–Φ30 | Φ4.3–Φ34 |
| Max thickness / width (mm) | 12 / 150 | 16 / 200 | 20 / 250 |
| Max horizontal bend (mm) | 150 / 12 | 200 / 16 | 250 / 20 |
| Max vertical bend size (mm) | 10×100 | 12×120 | 12×120 |
| Motor power | 3×4 kW | 3×5.5 kW | 3×5.5 kW |
FAT checks for punched busbars
- Hole diameters / oblong dims vs drawing
- Positions from datum (first / mid / last)
- Edge distance minimums
- Burr height and surface marks
- Deformation around dense hole fields
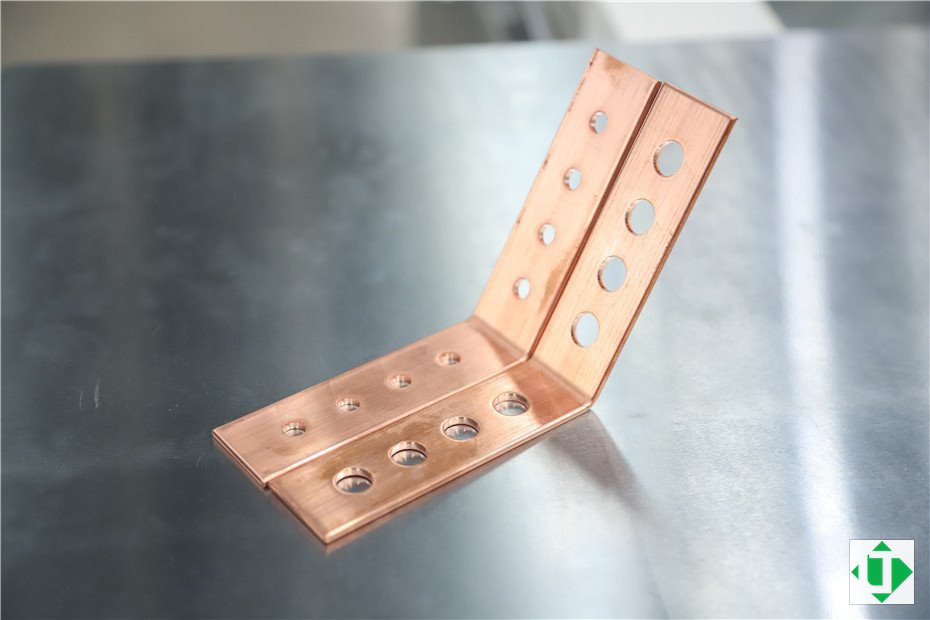
Copper samples after cut, punch and L-bend (LT / LTMC)
FAQ
What decides hole accuracy?
Datum discipline + positioning method + die condition + stable material—not a single brochure micron claim.
Can the same turret punch copper and aluminium?
Often yes with correct clearance and force margin. Re-qualify after material changes.
Round vs oblong dies?
Oblongs need matching die pairs and orientation control; list them explicitly in the RFQ.
Where does punching sit on a 3-in-1?
As an independent station beside shear and bend; three pump groups allow parallel work when staffed.
Talk to LT about a machine for your Australian workshop
For a quotation, FAT samples, tooling lists or sea freight to Australian ports (Sydney, Melbourne, Brisbane, Fremantle or Adelaide), contact LT at [email protected] or +86 13853146766 (WhatsApp), or use the contact page. Public product information is on busbarcnc.com.
Source and revision
- Prepared for: Australian switchboard builders and panel shops, published on busbarcnc.com
- Brand: LT / LTMC · models 303U-3-C · 503U-3-C · 803U-3-C
- Figures: LT / LTMC workshop photos and English schematics, hosted on this site
- Note: Confirm capacities, dies and voltages on the order acknowledgment and FAT samples. Electrical clearances in the finished assembly follow the switchgear design and AS/NZS 61439, not the machine alone.